Introduction
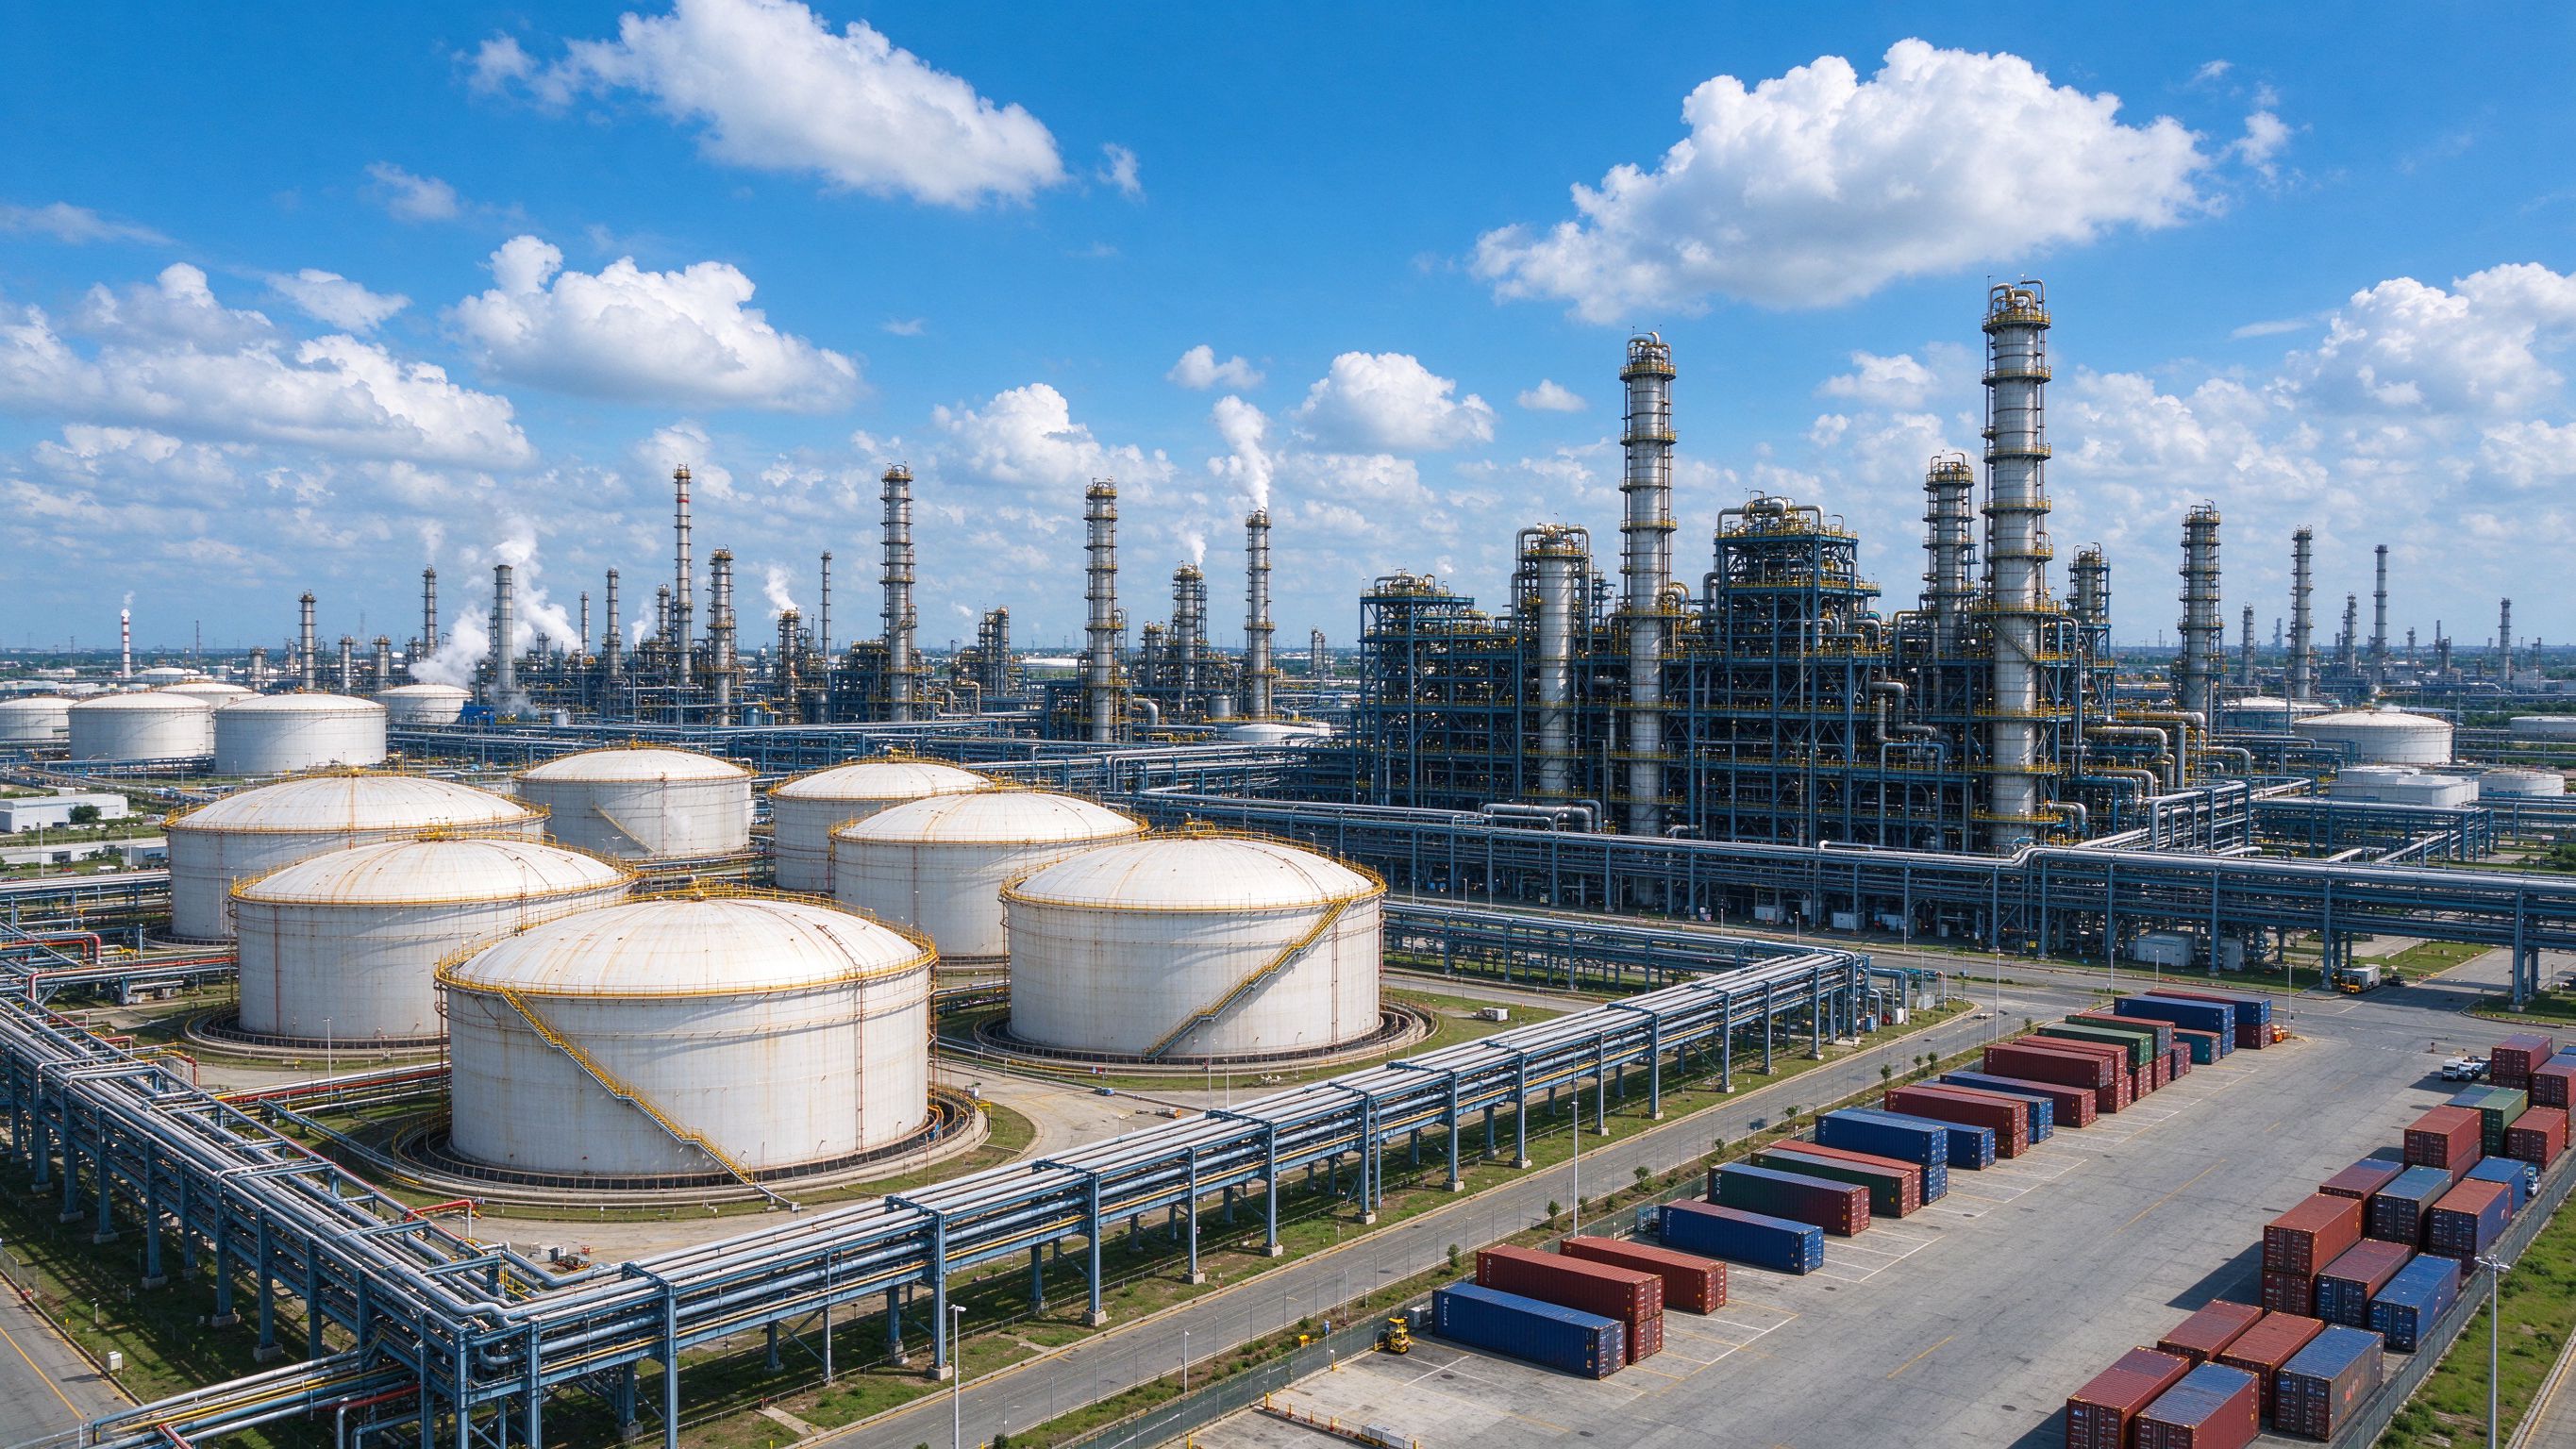
China has long been the world's manufacturing hub for fine and pharmaceutical chemical intermediates. For global buyers, the value of partnering with a China-based supplier extends well beyond price — it includes manufacturing depth, scale flexibility, and an increasingly professional export experience. This article examines the factors that make these partnerships successful.
1. Manufacturing Capability and Scale
Chinese chemical manufacturers benefit from mature supply chains, experienced process chemistry talent, and flexible production assets that can serve both research quantities and commercial volumes. This allows buyers to scale projects without changing suppliers.
2. Documentation and Compliance
Leading suppliers now meet international documentation expectations: COA, MSDS, NMR/LCMS data, and export documentation. Regulatory awareness has improved substantially, enabling smoother qualification and import processes for buyers.
3. The Partnership Model
Successful sourcing relationships are built on communication and transparency:
- Clear specifications agreed before production
- Regular quality updates and analytical data sharing
- Proactive logistics and customs support
- Flexible MOQ for R&D and scale-up
4. Sourcing Categories That Benefit
Fine chemical intermediates, pharmaceutical intermediates, OLED materials and organophosphorus compounds are among the categories where China-based suppliers offer strong capability. Buyers who qualify suppliers rigorously — on documentation, consistency and communication — unlock reliable, cost-effective supply.
Conclusion
China-based suppliers like Zhengzhou Whchem combine manufacturing capability, quality systems and export experience. For buyers seeking a dependable partner from gram to ton, the fundamentals are clear: verify quality, communicate specifications, and build long-term relationships.